2026 Best Milk Homogenizer What Is Its Role in Processing?

Time:2026-09-18 Author:Liam
0%

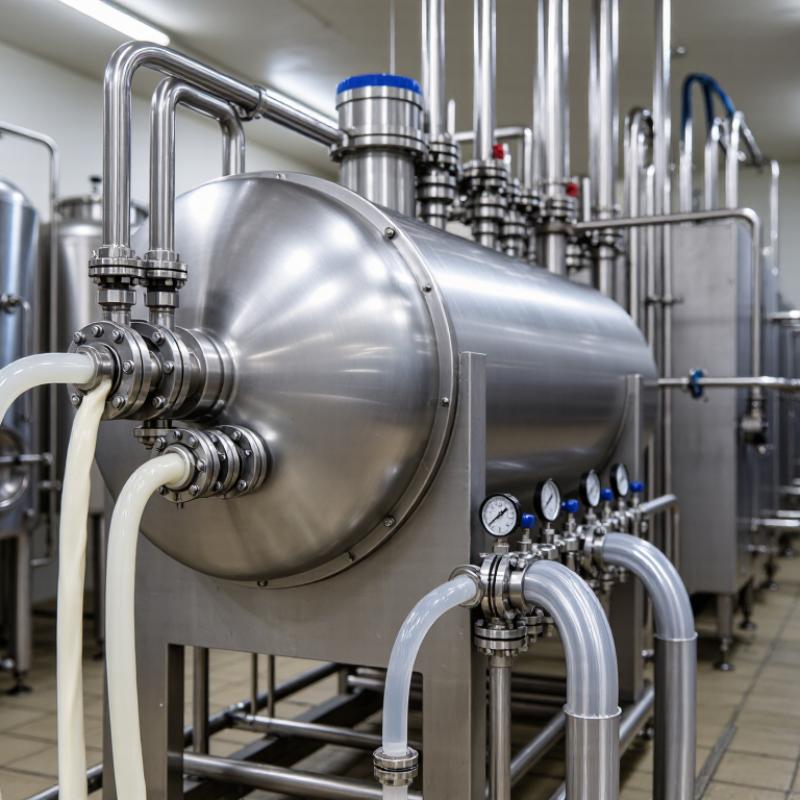
Choosing the 2026 best milk homogenizer requires more than comparing pressure ratings or stainless-steel finishes. A suitable machine must match milk composition, production volume, target texture, and cleaning procedures. In practical dairy operations, homogenization reduces fat globule size and helps prevent cream separation during storage. The result is smoother milk, a more consistent appearance, and improved consumer acceptance.

So, what is the role of homogenization in milk processing? It applies controlled mechanical force to milk, usually through a specialized valve and narrow flow passage. This action disperses fat more evenly throughout the liquid. Operators may notice the difference in a glass: the cream layer forms more slowly, while the mouthfeel becomes fuller and more uniform. However, homogenization is not a substitute for pasteurization, hygienic design, or strict temperature control. That distinction matters.

A reliable evaluation should consider capacity, operating pressure, seal durability, noise, energy use, and compatibility with clean-in-place systems. Validation should also include particle-size testing, microbiological controls, and long-term maintenance records. Experience shows that the highest pressure does not always deliver the best result. Excessive force can increase energy consumption and wear components unnecessarily. Sometimes, a modestly rated homogenizer performs better for a specific recipe. This is where product testing becomes essential. No single machine fits every dairy plant. The final decision should combine supplier documentation, operator feedback, service availability, and verified production data. Even well-designed equipment deserves regular review. Conditions change. Formulas change. Performance must be checked again.
2026 Best Milk Homogenizer What Is Its Role in Processing?

Milk Homogenization Explained: Reducing Fat Globules to Below 2 μm

2026 Best Milk Homogenizer: What Is Its Role in Processing?

Milk homogenization breaks large fat globules into much smaller particles, usually below 2 μm. Raw milk fat globules can range from about 0.1 to 15 μm, according to dairy science literature. Larger globules rise faster and form a cream layer. Homogenization limits this separation by forcing milk through a narrow valve under high pressure.

For fluid milk, industrial systems commonly operate around 100–250 bar. The pressure creates turbulence, shear, and cavitation near the valve. These forces reduce fat globule size and distribute milk fat more evenly.

The International Dairy Federation identifies homogenization as an important control for stable appearance, mouthfeel, and fat dispersion. Results still depend on temperature, pressure, fat content, and valve condition.

Small details matter. Milk is often homogenized near pasteurization temperatures, when fat is liquid enough to divide efficiently. Poor maintenance can create uneven particle sizes or excessive energy use. That assumption can fail.

FAO’s 2024 statistical reporting places global milk production at roughly 930 million tonnes in 2022. Such scale makes consistent processing essential, but volume alone does not prove quality. Operators should verify particle-size distribution, separation stability, and outlet temperature with documented tests. A milk homogenizer is not simply a high-pressure pump. It is a precision device, and the final result can change when one setting drifts.

How 15–25 MPa Pressure Stabilizes Milk Emulsions During Processing

2026 Best Milk Homogenizer: What Is Its Role in Processing?

Milk homogenization uses controlled pressure to make fat globules smaller and more evenly distributed. In many dairy applications, 15–25 MPa provides a practical working range. The milk passes through a narrow homogenizing valve, where turbulence, shear, and pressure release break larger fat globules apart. Smaller globules reduce creaming and help maintain a consistent appearance during storage.

Temperature matters greatly. Warm milk usually homogenizes more effectively because its fat phase becomes less viscous. Operators should also check inlet pressure, valve condition, and product flow. A pressure gauge may show 20 MPa, but worn valve parts can still create uneven treatment. That detail is easy to miss.

The result is a smoother emulsion with better physical stability. Milk remains visually uniform in the carton instead of forming a thick cream layer near the surface. However, pressure alone does not guarantee quality. Excessive pressure may increase energy use and influence protein interactions, especially in treated or fortified milk. Product composition changes the ideal setting. That assumption deserves testing.

A practical trial can compare 15, 20, and 25 MPa. Measure particle size, viscosity, and creaming after refrigerated storage. Record the milk temperature at every run. Small differences can reveal whether the homogenizer is truly stabilizing the emulsion or only compensating for poor process control.

2026 Best Milk Homogenizer: What Is Its Role in Processing? — How 15–25 MPa Pressure Stabilizes Milk Emulsions During Processing
Processing Dimension Typical Operating Range or Value Role in Milk Processing Effect on Emulsion Stability Practical Control Point
Homogenization pressure 15–25 MPa
150–250 bar
Forces milk through a narrow homogenizing valve, creating intense turbulence, shear, and cavitation. Breaks larger fat globules into a finer and more uniform dispersion, reducing the tendency of cream to rise. Pressure must be matched to fat content, solids level, temperature, and the desired product texture.
Milk temperature before homogenization Approximately 55–75°C for many conventional dairy applications Reduces fat viscosity and keeps milk fat sufficiently fluid during valve treatment. Supports efficient fat-globule disruption and improves the formation of a new interfacial layer around the smaller globules. Temperature is product-specific and should be coordinated with pasteurization or heat-treatment conditions.
Fat-globule size before treatment Native milk fat globules commonly range from about 0.1–15 μm, with a broad distribution. Represents the naturally variable dispersed-fat phase entering the homogenizer. Larger globules are more likely to cream during storage, especially when the serum phase is not sufficiently viscous. Raw-milk composition, animal factors, feed, season, and storage history can change the initial distribution.
Fat-globule size after homogenization Often reduced to a substantially finer distribution, commonly around 0.2–2 μm depending on equipment and formulation. Creates a larger total fat-surface area and a more uniform dispersed phase. Decreases visible creaming and improves consistency, opacity, and resistance to fat separation. Particle-size testing should use a defined analytical method because reported averages vary by measurement technique.
First-stage pressure Typically the main pressure stage, often within 15–25 MPa Performs most of the fat-globule size reduction through the primary homogenizing valve. Determines much of the product’s emulsion fineness and physical uniformity. Excessive pressure can increase energy use and may negatively affect viscosity or foaming in some formulations.
Second-stage pressure Commonly about 2–5 MPa when a two-stage system is used Helps reduce clustering of newly formed fat globules and moderates the flow leaving the first valve. Can improve storage stability and reduce the risk of re-agglomeration after primary homogenization. The optimum setting depends on milk composition, first-stage pressure, and the target product.
Milk-fat content Typical drinking milk may contain approximately 0.1–4.0% milk fat, depending on product category. Determines the amount of dispersed fat that must be processed. Higher fat loads generally require careful pressure and temperature control to maintain a stable emulsion. Reduced-fat and full-fat milks may require different homogenization settings for comparable stability.
Milk-solids and protein composition Whole milk commonly contains about 12–13% total solids; exact composition varies. Milk proteins, especially casein and whey proteins, adsorb at the newly created fat-water interface. Protein coverage helps prevent fat-globule coalescence and contributes to a stable emulsion. Changes in protein level, added ingredients, or heat treatment can alter viscosity and homogenization response.
Number of homogenization passes Usually one pass; two-stage treatment is also widely used. Controls the amount of mechanical processing applied to the milk. A properly selected pass configuration can provide uniformity without unnecessary shear, heat generation, or energy consumption. Multiple passes should be validated because additional processing does not automatically produce better stability.
Emulsion-stability indicators Low visible cream separation, consistent particle-size distribution, and stable viscosity during storage Shows whether the homogenizer has produced a sufficiently uniform fat dispersion. Stable emulsions maintain a more consistent appearance, mouthfeel, and composition throughout shelf life. Evaluate stability under defined storage time and temperature conditions rather than relying on pressure alone.
Microbial control Homogenization is a physical treatment and does not replace pasteurization or sterilization. Reduces fat-globule size but does not reliably destroy pathogenic microorganisms. Emulsion stability and microbiological safety are separate performance objectives. Use validated heat-treatment, hygienic-design, cleaning, and cold-chain procedures alongside homogenization.
Energy and process impact Higher pressure generally increases mechanical energy input and can raise product temperature. Provides stronger disruption of the dispersed fat phase but increases operating demand. Correctly selected pressure balances stability, texture, throughput, and energy efficiency. Monitor inlet temperature, outlet temperature, pressure fluctuation, flow rate, and valve condition.

Note: The values shown are representative technical ranges for conventional dairy processing, not universal specifications. Final settings should be confirmed through product-specific trials, particle-size analysis, storage testing, and applicable food-safety requirements.

Homogenizer Designs Compared: Two-Stage Systems for Commercial Dairy Lines

2026 Best Milk Homogenizer: What Is Its Role in Processing?

Milk homogenization reduces fat globules and helps prevent cream separation during storage. The OECD-FAO Agricultural Outlook 2024–2033 projects global milk production to grow about 1.6% annually. This pressure makes stable, efficient dairy lines increasingly important. A homogenizer also improves mouthfeel, whiteness, and product consistency. However, it cannot repair poor raw milk quality or weak sanitation.

Two-stage systems are widely considered for commercial dairy lines. The first stage applies most of the pressure and breaks large fat globules. The second stage reduces remaining clusters and limits recombination. This design can produce smoother drinking milk, creamier cultured products, and better shelf stability.

It may also require more energy, maintenance, and careful valve adjustment. Single-stage units can be suitable for simpler products or smaller throughputs. The two-stage option is not automatically better. Product viscosity, fat level, inlet temperature, and target shelf life must guide the decision.

Tips: Check particle-size results, not pressure alone. Review energy use per tonne. Inspect valve wear during real production trials. The International Dairy Federation emphasizes process control, hygiene, and validated operating conditions across dairy manufacturing. Operators should record pressure, temperature, flow rate, and separation results each shift. Small variations matter. A practical concern remains: laboratory smoothness may not match texture after transport, storage, and repeated temperature changes.

How Homogenization Improves Creaminess, Shelf Stability, and Pouring Consistency

Homogenization gives milk a smoother, creamier mouthfeel by breaking large fat globules into much smaller particles. Technical reviews in the Journal of Dairy Science report typical homogenized globules below 1 micrometre, compared with several micrometres in untreated milk. This finer dispersion slows cream separation. It also creates a more uniform white appearance and steadier pouring from the first glass to the last.

Shelf stability improves, but homogenization is not sterilization. The FAO Dairy Development Guide explains that homogenization supports emulsion stability, while heat treatment controls most microbial risks. Processing pressure commonly ranges from 100 to 250 bar, depending on fat content, temperature, and equipment design. Excessive pressure can increase foaming or oxidation. That detail is easy to overlook. Pouring consistency also depends on cooling speed, storage temperature, and protein balance, not the homogenizer alone.

Tips: Keep the milk near its designed processing temperature, check valve wear, and measure fat separation after storage. A practical test is simple: refrigerate samples for 48 hours, then compare the cream line and pouring flow. Results may vary between batches. That is not failure; it is a signal to review pressure, inlet temperature, and oxygen exposure. Industry processing reports consistently treat these variables as a connected system, rather than isolated machine settings.

Choosing the Best 2026 Milk Homogenizer by Capacity, Energy Use, and CIP Needs

In 2026, the best milk homogenizer is not automatically the largest or fastest machine. Its role is to reduce fat globules and distribute them evenly, improving cream stability, mouthfeel, and product consistency. In practical plant work, capacity should match the real production rhythm, not an optimistic target. A unit running near its limit may increase pressure fluctuations, heat, and maintenance demands. Oversizing also wastes capital and energy. That choice is easy to underestimate.

For capacity, compare hourly flow with batch size, peak demand, and future expansion. A dairy processing 2,000 liters per hour needs a different configuration from a high-volume continuous line. Ask for performance data at the intended pressure and milk temperature. Energy use depends on motor efficiency, operating pressure, product viscosity, and idle time. Lower pressure is not always better; insufficient pressure can weaken dispersion. Metering actual electricity during trials is more useful than trusting a brochure estimate. A small test can expose uncomfortable assumptions.

CIP needs deserve equal attention. Select hygienic contact surfaces, drainable piping, suitable seals, and verified cleaning coverage. Confirm flow velocity, chemical compatibility, cleaning temperature, and rinse-water demand with the equipment supplier and sanitation team. A homogenizer that cleans slowly can delay production and raise water consumption. Automated monitoring helps record pressure, temperature, and cleaning cycles, supporting traceability and preventive maintenance. Still, sensors can drift. Operators should review unusual readings instead of accepting every value. The best 2026 choice balances throughput, energy, cleanability, service access, and measured results—not impressive specifications alone.

FAQS

What pressure range is commonly used for milk homogenization?

A practical range is 15–25 MPa, or about 150–250 bar. The best setting depends on fat content, temperature, and equipment design. Pressure alone is not enough.

How does homogenization reduce cream separation?

Milk passes through a narrow valve under pressure. Turbulence and shear break large fat globules into smaller particles. These particles remain distributed longer, reducing the visible cream layer.

Why does processing temperature matter?

Warm milk usually homogenizes more effectively because its fat phase becomes less viscous. Operators should record temperature during every production run. Small temperature changes can matter.

Can higher pressure always improve milk quality?

No. Excessive pressure may increase energy use, foaming, or oxidation. It can also change protein interactions in treated or fortified milk. The “higher is better” idea needs testing.

What is the difference between one-stage and two-stage homogenization?

A one-stage system may suit simpler products and smaller production volumes. A two-stage system uses a second pressure step to reduce remaining clusters. It may create smoother texture, but requires more energy and maintenance.

What measurements should operators check besides pressure?

Check particle size, viscosity, temperature, flow rate, valve condition, and cream separation. Energy use per tonne also deserves attention. A pressure gauge can look normal while worn valves create uneven treatment.

How can a dairy processor test homogenization performance?

Compare samples processed at 15, 20, and 25 MPa. Measure particle size, viscosity, and cream formation after refrigerated storage. A simple 48-hour test can reveal meaningful differences.

Does homogenization sterilize milk?

No. Homogenization improves emulsion stability, not microbial safety. Heat treatment and sanitation control most microbial risks. That distinction is easy to forget.

Why might milk pour differently after storage or transport?

Cooling speed, storage temperature, protein balance, and oxygen exposure affect pouring consistency. Repeated temperature changes may alter the final texture. Laboratory smoothness is not always the carton experience.

What should operators do when batches produce different results?

Review pressure, inlet temperature, flow rate, valve wear, and raw milk quality. Record these conditions each shift. Variation is not automatically failure. It is a warning.

Conclusion

Milk homogenization is a key step in modern dairy processing that breaks large fat globules into particles typically smaller than 2 μm. By applying approximately 15–25 MPa of pressure, the process creates a more stable emulsion, helping prevent cream separation and improving the uniformity of milk during storage, transportation, and serving. This explains what is the role of homogenization in milk processing: it enhances texture, creaminess, shelf stability, and pouring consistency without changing the basic nature of the product.

For commercial dairy operations, two-stage homogenizer systems are often preferred because they provide effective particle size reduction and better emulsion control across continuous production lines. When selecting the best milk homogenizer for 2026, processors should evaluate production capacity, energy consumption, pressure flexibility, maintenance requirements, and compatibility with clean-in-place (CIP) procedures. The right equipment can support consistent quality while improving operational efficiency and hygiene management.
Liam

Liam

Liam is a dedicated marketing professional with a profound expertise in the industry, where he excels at highlighting the unique advantages of our core products. With a keen understanding of market trends and consumer needs, Liam frequently updates our company’s professional blog, providing......