Engineered for absolute hygienic integrity, continuous production throughput, and full compliance with international HACCP and GMP standards.
The global food and beverage processing sector is experiencing an unprecedented structural transformation driven by tightening international regulatory frameworks, shifting consumer preferences for clean-label products, and the imperative to mitigate food safety risks across complex cross-border supply chains. Modern food manufacturing no longer views quality control (QC) as a static end-of-line verification step. Instead, leading enterprise processors adopt real-time, inline, and continuous quality assurance (QA) frameworks embedded directly within high-speed automated processing machinery.
In this evolving landscape, China has emerged as the premier global powerhouse for wholesale food quality control equipment manufacturing and custom machinery engineering. Driven by large-scale industrialization and massive investment in Industry 4.0 integration, Chinese OEM/ODM suppliers provide global food processors with access to state-of-the-art vision inspection, inline foreign body detection, aseptic packaging isolators, and automated fruit/vegetable processing lines at competitive capital expenditure (CapEx) levels.
Strategic Information Gain: Transitioning from manual spot-checking to automated inline inspection yields an average of 42% reduction in product waste, 99.98% contamination detection accuracy, and full regulatory traceability under US FDA FSMA, EU 1935/2004, and global HACCP mandates.
To understand the competitive edge offered by leading Chinese manufacturers, enterprise procurement teams must evaluate the key technological shifts defining contemporary food processing equipment:
Combining traditional optical sorting with Near-Infrared (NIR) multi-spectral cameras to detect internal decay, sugar content (Brix), moisture distribution, and non-visible surface defects in fresh produce and liquid lines.
Integration of Modbus TCP/IP, OPC UA, and cloud-connected PLC controllers allowing real-time monitoring of critical control points (CCPs), temperature deltas, flow dynamics, and vibration analysis for predictive maintenance.
Engineering compliance with EHEDG and 3-A Sanitary Standards. Equipment utilizes seamless continuous welds, IP69K washdown enclosures, and fully automated Clean-in-Place (CIP) and Sterilize-in-Place (SIP) systems.
Global procurement directors evaluate equipment suppliers based on total lifecycle value, operational efficiency, and rapid return on capital investment.
China's manufacturing ecosystem for food processing and quality control equipment has undergone a remarkable evolution. The industrial cluster in Guangdong Province, particularly centered in Dongguan City, represents a high-density hub of engineering design, precision CNC machining, electrical automation assembly, and international logistics integration.
By leveraging an intact component supply chain—ranging from food-grade 316L stainless steel procurement to localized production of high-precision pneumatics and optical sensors—Chinese manufacturers offer unmatched lead time advantages, flexible OEM/ODM custom engineering, and superior total cost of ownership (TCO).
Dongguan CarniTe Machinery Co., Ltd. Company Benchmark: As a dedicated industrial pioneer, CarniTe Machinery integrates end-to-end processing equipment manufacturing with automated quality control systems, providing turnkey engineering solutions to over 50 countries worldwide.
Dongguan CarniTe Machinery Co., Ltd. is a professional manufacturer specializing in fruit and vegetable processing equipment and integrated industrial food processing solutions. The company focuses on the research, development, production, and global supply of advanced processing lines for fruits, vegetables, and related food products. With strong engineering capability and industry experience, CarniTe Machinery delivers turnkey solutions that ensure efficient, hygienic, and scalable food production.
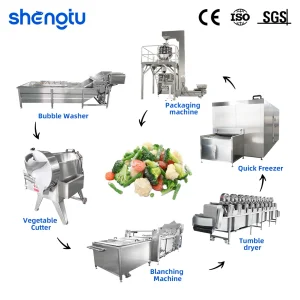
Core systems include washing, sorting, peeling, cutting, juicing, pulping, blanching, freezing, drying, and packaging lines, widely applied in food factories, beverage plants, and agricultural processing industries. The company is committed to improving production efficiency, reducing labor costs, and maintaining consistent product quality through automation and intelligent control technologies.
Dongguan CarniTe Machinery Co., Ltd. maintains strict quality standards and complies with international manufacturing requirements. It provides OEM and ODM customization services tailored to different capacities and production needs. By combining innovation, reliability, and customer-focused engineering, the company continues expanding into Asia, Europe, the Middle East, and the Americas, aiming to become a trusted global partner in food processing automation.
The company also invests heavily in research and development, continuously upgrading processing technology, improving energy efficiency, and enhancing equipment stability, while providing comprehensive after-sales support, installation guidance, and technical training to ensure long-term operational success for global customers in diverse food manufacturing environments.
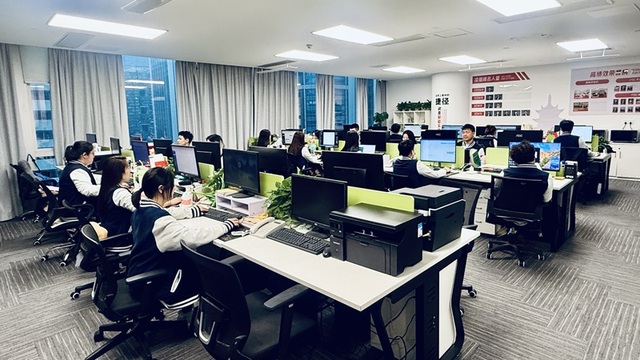
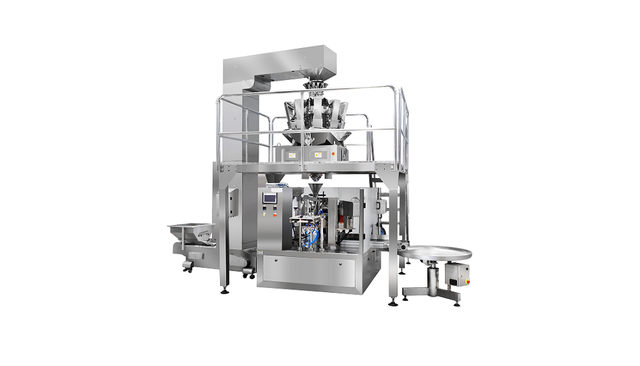
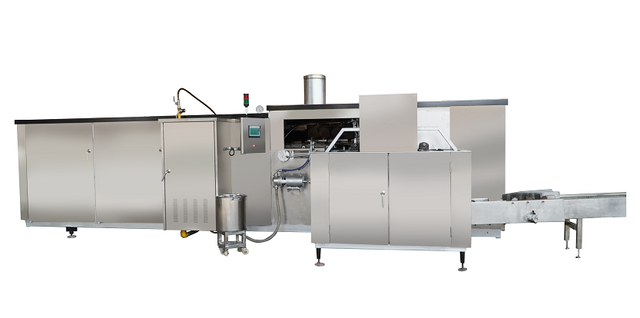
Below is an overview of our state-of-the-art manufacturing facility, machining capabilities, assembly workshops, and quality testing standards:
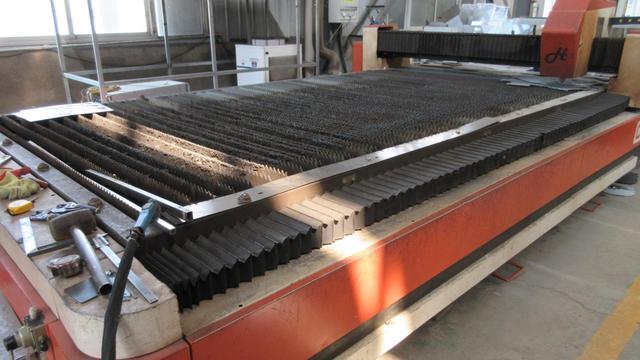
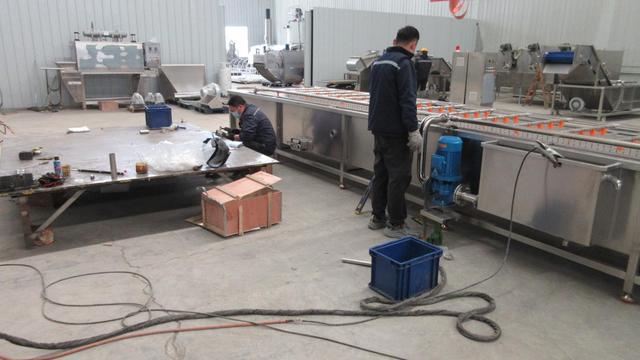
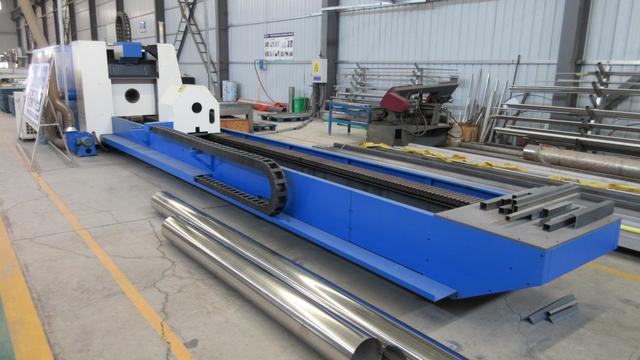
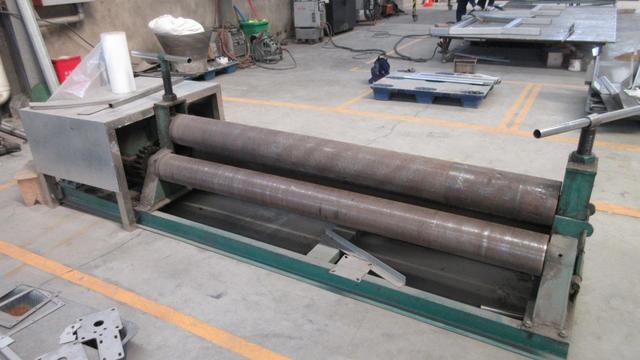
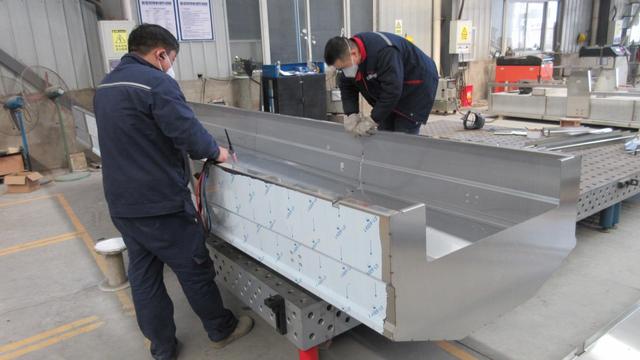
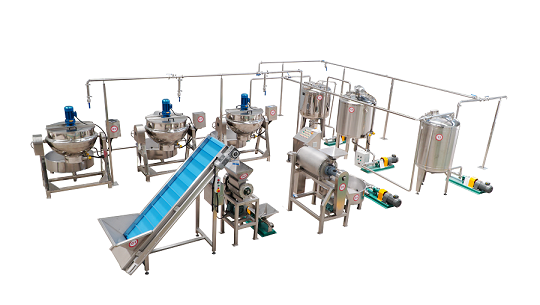
Different sectors of the food, beverage, and agricultural processing industries demand tailored technological architectures. Modern food factory managers must carefully match quality control and processing machinery with specific product physical characteristics, hygiene classes, and throughput rates.
| Industry Sector | Primary Quality Risks | Recommended System Architecture | Compliance & Standard Target |
|---|---|---|---|
| Fresh Produce & Post-Harvest | Bruising, rot, color imbalance, foreign stone/soil contamination | Optical Vision Sorting, Multi-stage Washing & Brush Peeling Lines | GlobalGAP, ISO 22000, HACCP CCP1 |
| Beverages, Beer & Juices | Brix variation, fill level errors, cap torque failure, micro-contamination | Automated Carbonators, Inline Flowmeter Fillers, Capping Inspection | FDA Beverage HACCP, CE Certification |
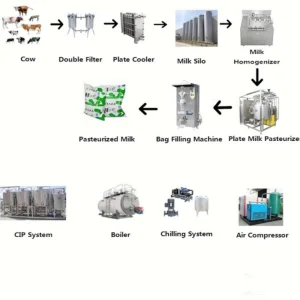
| Dairy & Frozen Foods | Bacterial growth, listeria, texture loss, incomplete freezing | Pasteurization Lines, IoT IQF Tunnel Freezing, Hygienic Piping | 3-A Sanitary Standards, EHEDG |
| Aseptic Pharma & Bio-Formulation | Particulate ingress, batch cross-contamination, sterility breach | Aseptic Filling Isolators, GMP Vaccine Blending Tanks | EU GMP Annex 1, US FDA 21 CFR Part 11 |
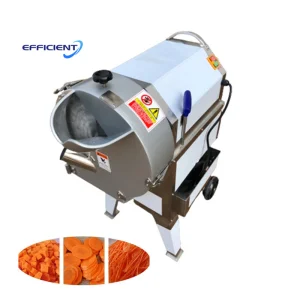
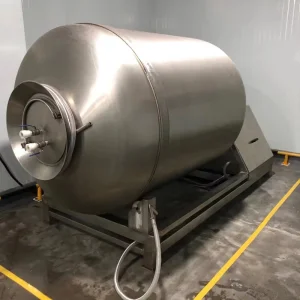
| Meat & Processed Vegetables | Uneven pickling/marination, slice thickness variation, bone fragments | Large-Scale Vacuum Rolling Machines, High-Speed Precision Dicers | USDA Organic, HACCP Metal/X-Ray CCP |
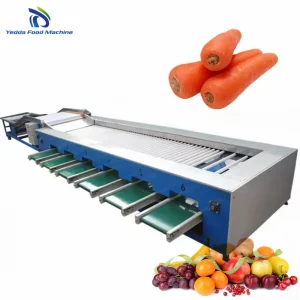
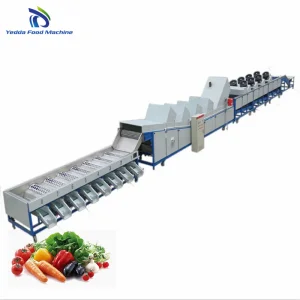
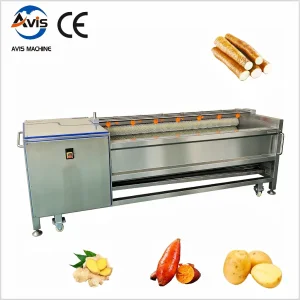
Post-harvest management requires immediate sorting and continuous washing to prevent fungal spoilage. Modern fruit sorting lines integrate weight, optical color sizing, and automated defect rejection mechanisms. Paired with multi-functional brush washing and cassava/potato peeling equipment, processors achieve maximum yield recovery while significantly reducing manual hand-sorting overhead.
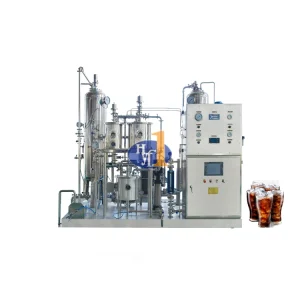
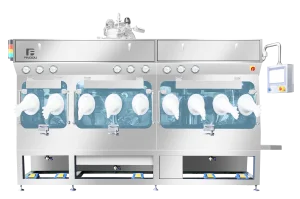
High-speed liquid processing demands precise gas-liquid ratio control. Automated carbonation systems use mass flow controllers to ensure stable CO2 volume dissolution in soft drinks and beer lines. Continuous liquid bottling, automated capping, and aseptic filling isolators protect delicate formulations from atmospheric airborne particles, essential for both beverage security and bio-pharmaceutical liquid blending.
Detailed technical answers to common queries regarding wholesale machinery procurement, custom OEM engineering, international compliance, and technical support.
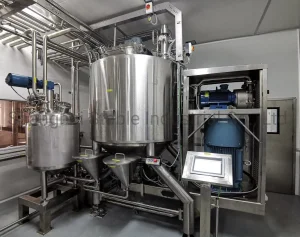
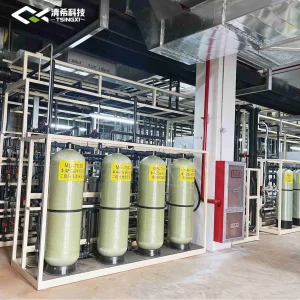
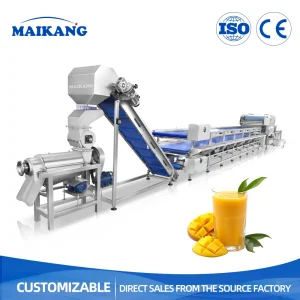
Explore our full operational portfolio of vacuum homogenizers, water treatment RO systems, dairy lines, and automated vegetable processing plants.
 CarniTe Machinery